Overview & Strategic Context
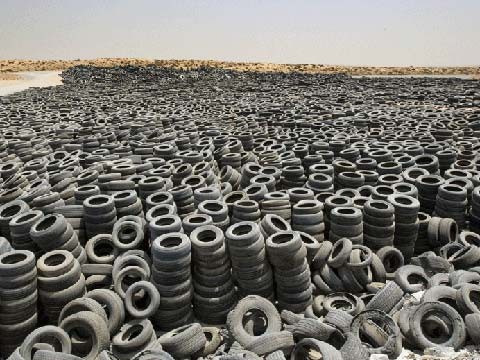
Discarded vehicle tyres create persistent fire hazards and harbor disease vectors if stockpiled outdoors. Shree Alliance operates an environmentally sealed vacuum pyrolysis and cryogenic granulation system that recovers 100% of tyre components into valuable industrial products. Our continuous pyrolysis unit operates without smoke or harmful emissions, yielding heavy industrial fuel oil, recovered carbon black (rCB), and high-tensile steel wire.
Technical Process & Circular Recovery Flow
Tyre Debeading & Primary Shredding
Hydraulic pullers cleanly extracting high-tensile bead wires before heavy shredders reduce tyres into uniform rubber chips.
Continuous Indirect Catalytic Pyrolysis
Sealed, oxygen-free thermal reactors decomposing rubber hydrocarbons into combustible oil vapors and carbon black char.
Hydrocarbon Condensation & Gas Recycling
Heat exchangers condensing oil vapors into pyrolysis fuel oil, while non-condensable syngas loops back to fire the reactor.
Carbon Black Milling & Micronization
Magnetic purification and jet milling refining recovered carbon black into masterbatch-grade industrial pigment.
Key Recovered Materials & Commercial Outputs
Statutory Compliance & EPR Framework
Regulatory Standards: Approved continuous catalytic pyrolysis adhering to CPCB Standard Operating Procedures (SOP), strict air pollution control scrubbers, and zero water pollution.